 | AboutDONSIN|Blog|Teachless Robotic Welding for H-Beams and Steel Structures: DONSIN RA Series Explained
Teachless Robotic Welding for H-Beams and Steel Structures: DONSIN RA Series Explained
Nov. 09, 2026
In a steel structure workshop, the slow part of robotic welding is often not the welding. It is the teaching. Every column, roof beam and crane beam has stiffeners, end plates and connection plates in slightly different places. If a programmer must teach every point for every variant, the robot spends more time waiting than welding.
This is the problem teachless robotic welding is designed to solve. Here is how it works in the DONSIN RA series, and how to choose between the four models.
1. What "teachless" really means
In a conventional robot cell, someone moves the arm to each weld start and end point and records the path. In a teachless system, the cell recognizes the workpiece, locates the weld seams and generates the welding path automatically.
DONSIN's RA series uses a 3D teach-free welding system (BOCHU) that identifies the workpiece, detects the seams and builds the path. It is aimed at large structural components with many welds, where manual teaching would be the bottleneck.
Teachless does not mean "no preparation." The robot still needs parts that are positioned reasonably, tacked correctly and clean at the joint. What changes is who does the work: the system generates the path, and the operator checks and confirms it.
2. Anatomy of an RA cell
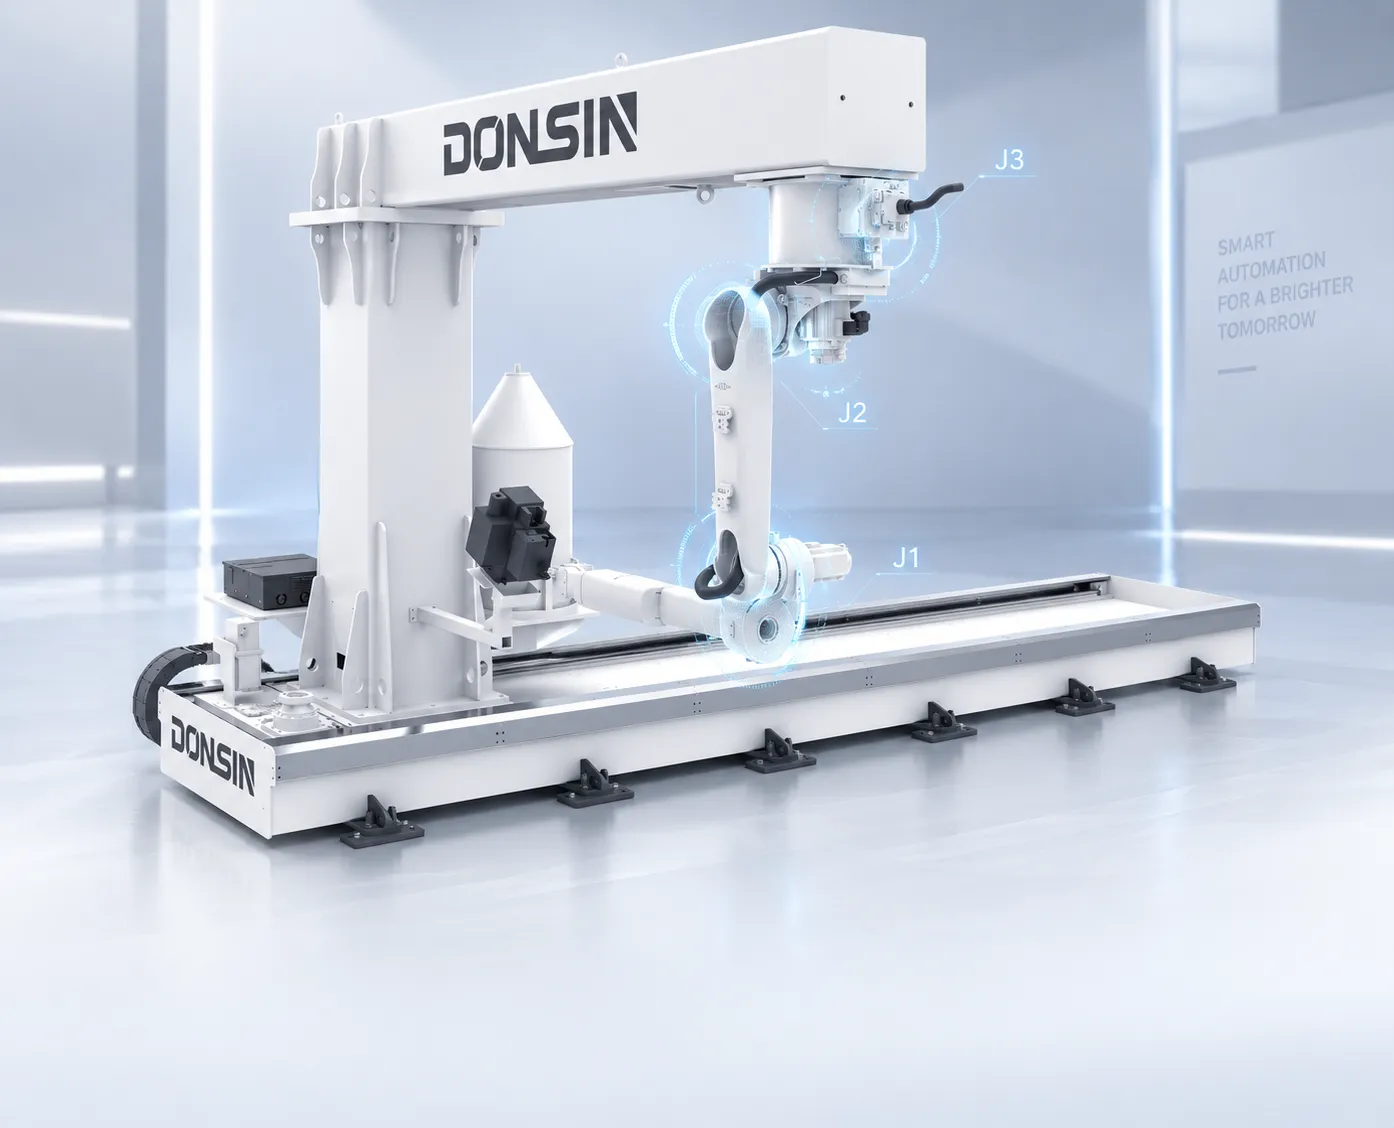
An RA robotic welding arm is a track-based industrial system. The common elements are:
- A 6 kg payload, 2014 mm reach robot arm with ±0.08 mm repeatability
- A 500 A welding source (Megmeet)
- A floor-mounted track (X-axis) with an effective stroke of up to 10 to 12 meters, so the robot travels along the length of the beam
- Optional cantilever axes that extend lateral reach or rotate the arm
- A modular workstation, with optional vision, torch cleaning and welding peripherals
The result is a welding robot arm that moves to the work, instead of requiring you to move heavy members to the robot.
3. The four RA models compared
| RA-S7 | RA-S7Pro | RA-S8 | RA-S8Pro | |
|---|---|---|---|---|
| Structure | Floor track | Floor track + cantilever | Floor track + cantilever Y-axis | Floor track + cantilever A-axis |
| Total axes | 7 | 7 | 8 | 8 |
| X-axis load | 1000 kg | 1000 kg | 4000 kg | 5000 kg |
| X-axis stroke | ≤ 12,000 mm | ≤ 10,000 mm | ≤ 10,000 mm | ≤ 10,000 mm |
| X-axis max speed | 50 m/min | 45 m/min | 30 m/min | 30 m/min |
| X-axis positioning accuracy | ±0.1 mm | ±0.05 mm | ±0.05 mm | ±0.05 mm |
| Y-axis stroke | none | none | 2000 mm | none |
| A-axis rotation | none | none | none | 180° |
| Approx. footprint | 14,000 × 3,000 × 3,000 mm | 11,600 × 4,500 × 6,000 mm | 11,600 × 4,500 × 6,000 mm | 11,600 × 4,500 × 6,000 mm |
All four share the same 500 A source, 2014 mm arm reach, 6 kg payload and ±0.08 mm arm repeatability.
4. How to choose between them
RA-S7: the straightforward, long-travel option. With a stroke up to 12 meters and the fastest travel speed, it suits open members where the robot can reach the joints from one side of a long beam.
RA-S7Pro: tighter positioning and cantilever access. Travel accuracy improves to ±0.05 mm and a cantilever structure helps reach, at slightly shorter stroke and speed.
RA-S8: for heavier and wider parts. The 8th axis adds a 2000 mm Y-axis travel and a 4000 kg X-axis load. DONSIN notes that the added lateral travel reduces repeated lifting and repositioning of the workpiece, and that multi-zone welding lets a single system cover several areas of a large structure.
RA-S8Pro: for the heaviest work and the most joint orientations. It carries up to 5000 kg and adds an A-axis with up to 180° of rotation. Ask DONSIN how this axis would be used on your specific parts.
A practical rule: choose by the heaviest member you handle and by how many sides of it must be welded without turning it over.
5. Which parts is it designed for?
DONSIN positions the RA series for fillet welds on light steel structures, such as H-section columns, roof beams and crane (runway) beams, particularly relatively open members.
Be realistic about scope. A system designed for fillet welds on open sections is not automatically the right choice for every steel job. If you weld enclosed box sections, very thick plate with deep multi-pass grooves, or heavy girders with complex access, discuss the joint types with DONSIN and run a trial before committing.
6. What a typical workflow looks like
- Load the beam or column onto the supports.
- Scan the workpiece so the system identifies the part and its seams.
- Review the generated welding paths and parameters.
- Weld along the track, with the robot moving from zone to zone.
- Unload and inspect while the next part is prepared.
The value is largest when you have many similar structural members with changing details, because the time saved is in the programming step you no longer do by hand.
7. What decides quality in a teachless cell
The scanner finds seams. It cannot fix a poorly prepared joint. For consistent results:
- Keep fit-up gaps within a controlled range.
- Tack parts consistently and avoid parts that can shift.
- Clean the joint area of heavy scale, oil and contamination.
- Define welding parameters for each joint type and leg size, and verify them with a test piece.
- Follow the welding procedure requirements that apply to your project.
8. Planning the installation
These systems are substantial. The S7 occupies about 14 × 3 × 3 m, while the S7Pro, S8 and S8Pro are about 11.6 × 4.5 × 6 m. Check floor space, ceiling height, crane access for loading beams, and the 380 V three-phase supply. DONSIN lists operating conditions of −10 to 45 °C, 20–80% humidity, and vibration up to 4.9 m/s².
9. RA or RW?
If you weld small and medium parts in changing batches, a collaborative RW system may be easier to deploy. If your core work is long, heavy, repeatable steel members, a track-based RA cell is designed for that scale. Many fabricators run both.
10. Prepare these for a quote
- Drawings of typical beams and columns
- Section sizes, lengths and weights
- Weld leg size and material grade
- Monthly volume and variety of part types
- Workshop dimensions and crane capacity
The takeaway
A teachless robotic welding arm removes the programming bottleneck in steel structure fabrication. The right RA model depends on part weight, how many sides must be welded, and how far the robot must travel. Confirm it with a test on your own members.
Welding H-beams or light steel structures?Send us your drawings and we will recommend a configuration.
Request a Welding Solution →


